Manufacturing
The Paver Block
Manufacturing Process
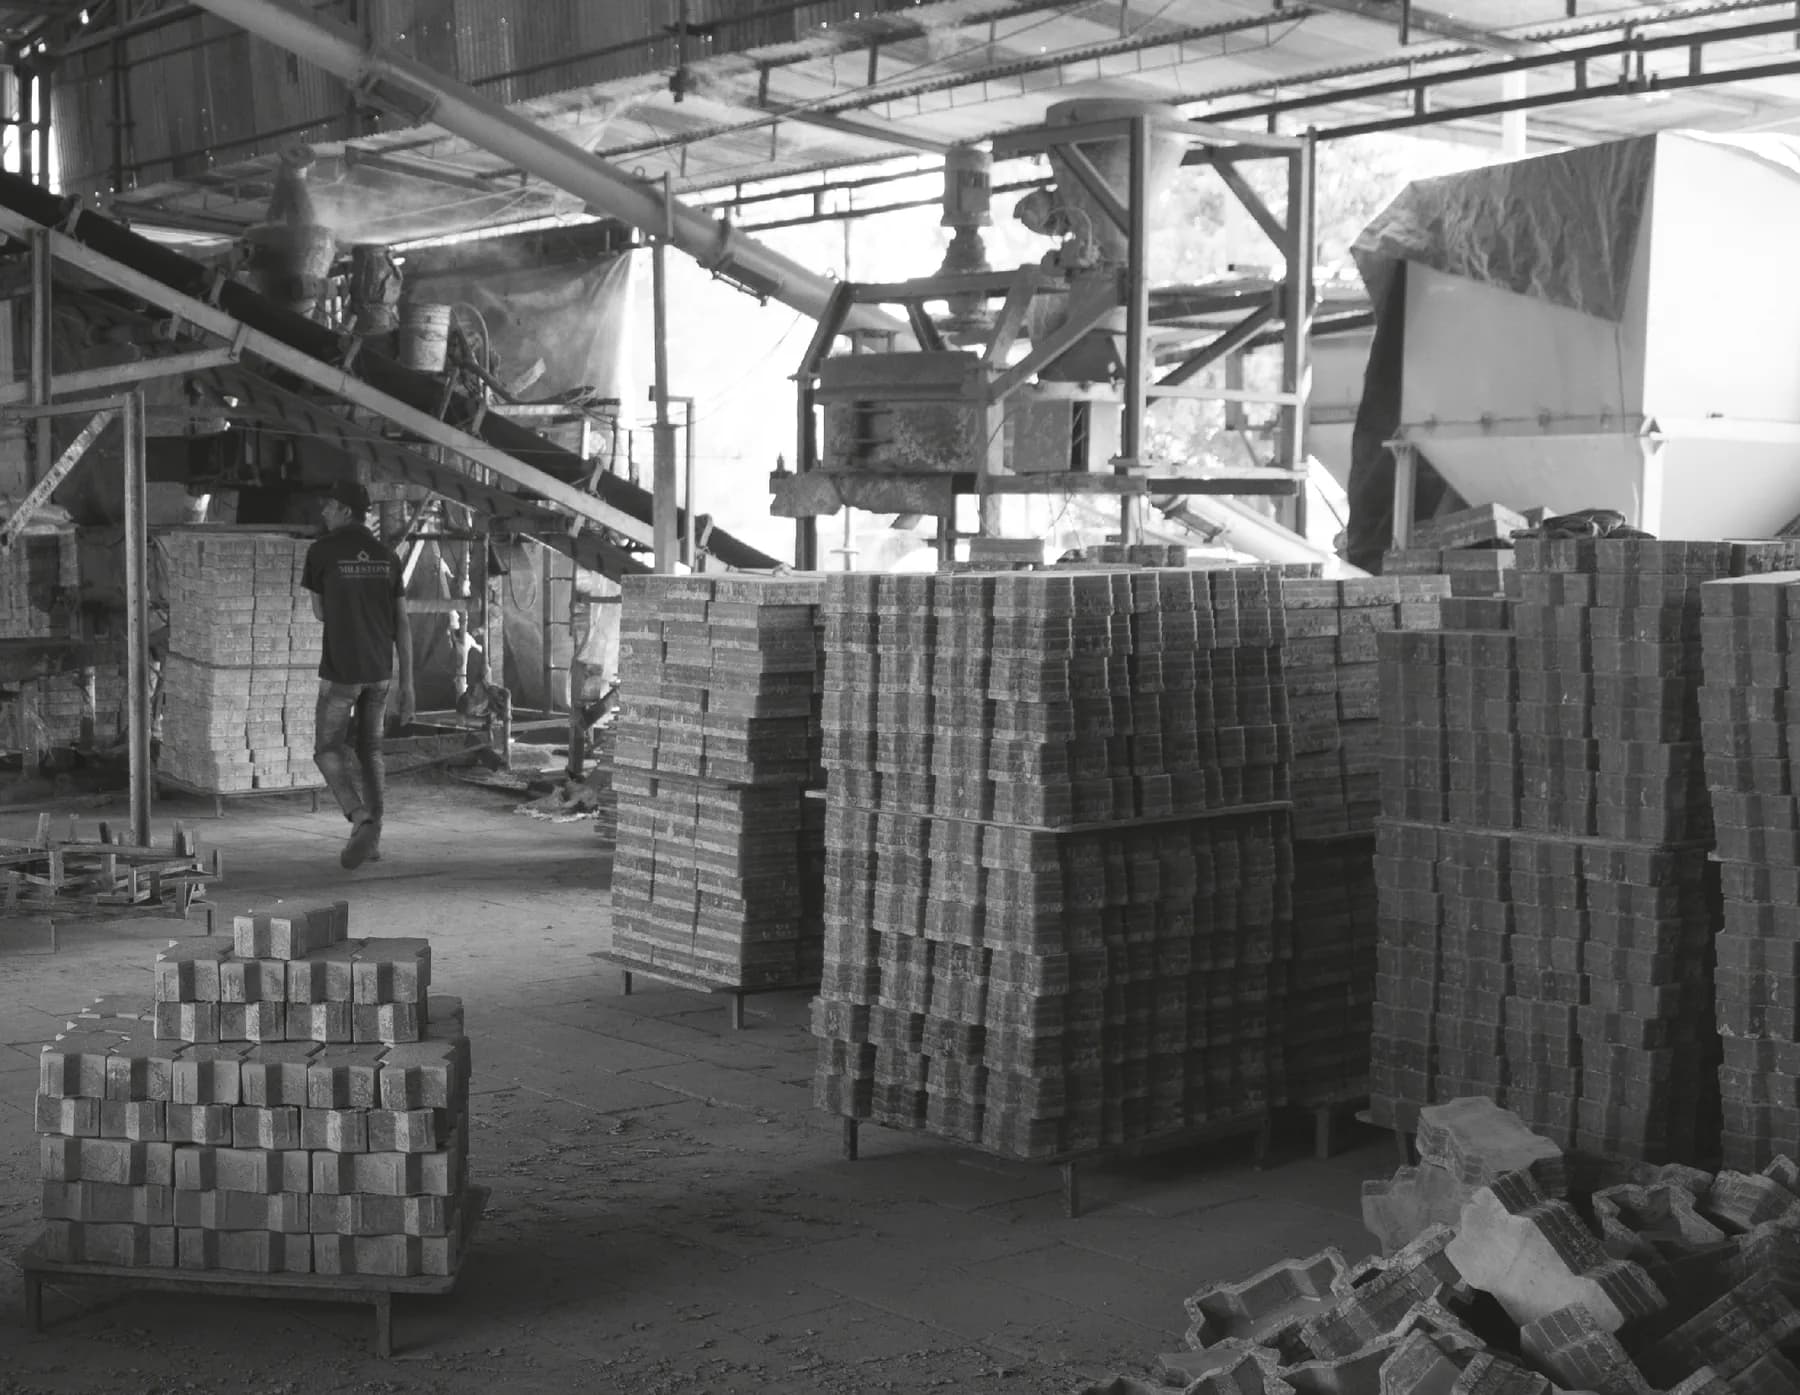
Every Milestone product is made in-house at our own factory in Bavla, Ahmedabad — from automated production and steam curing to in-house quality testing and our own delivery fleet.
1
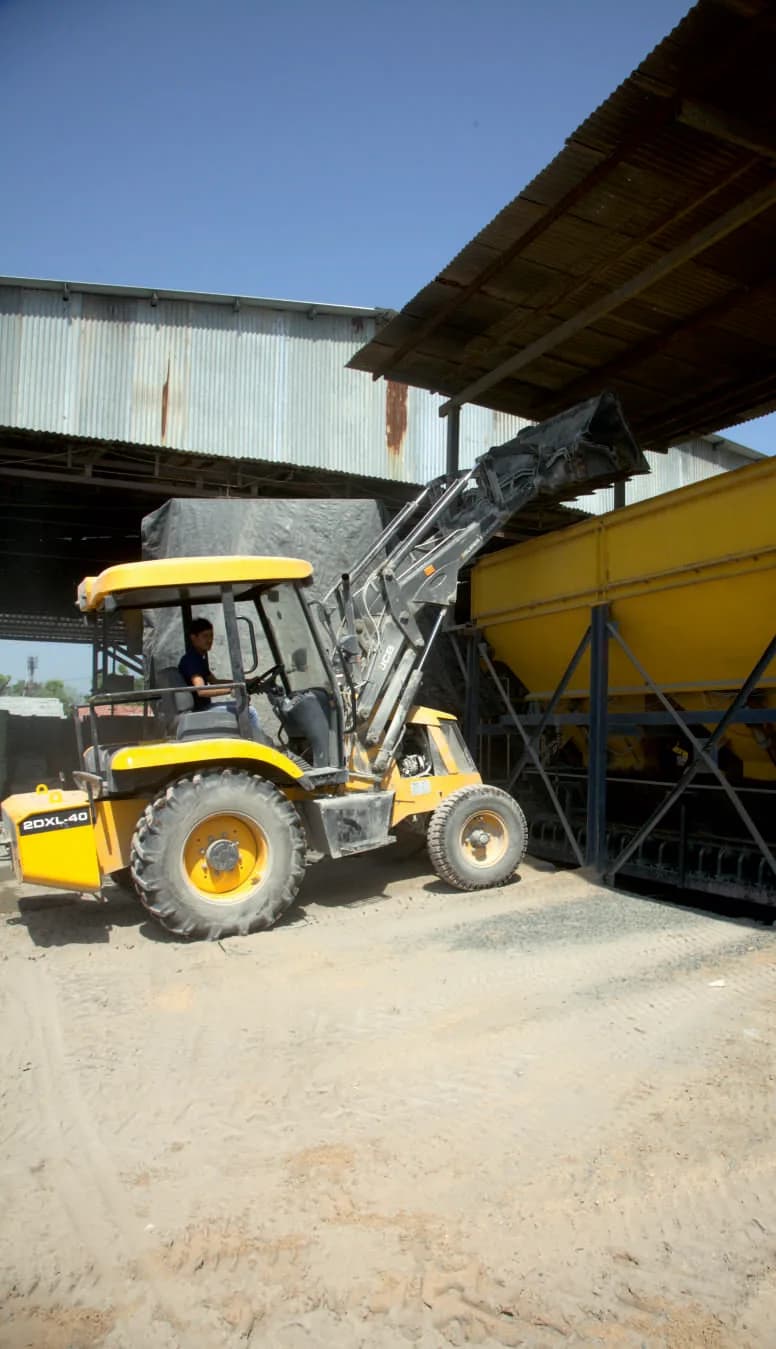
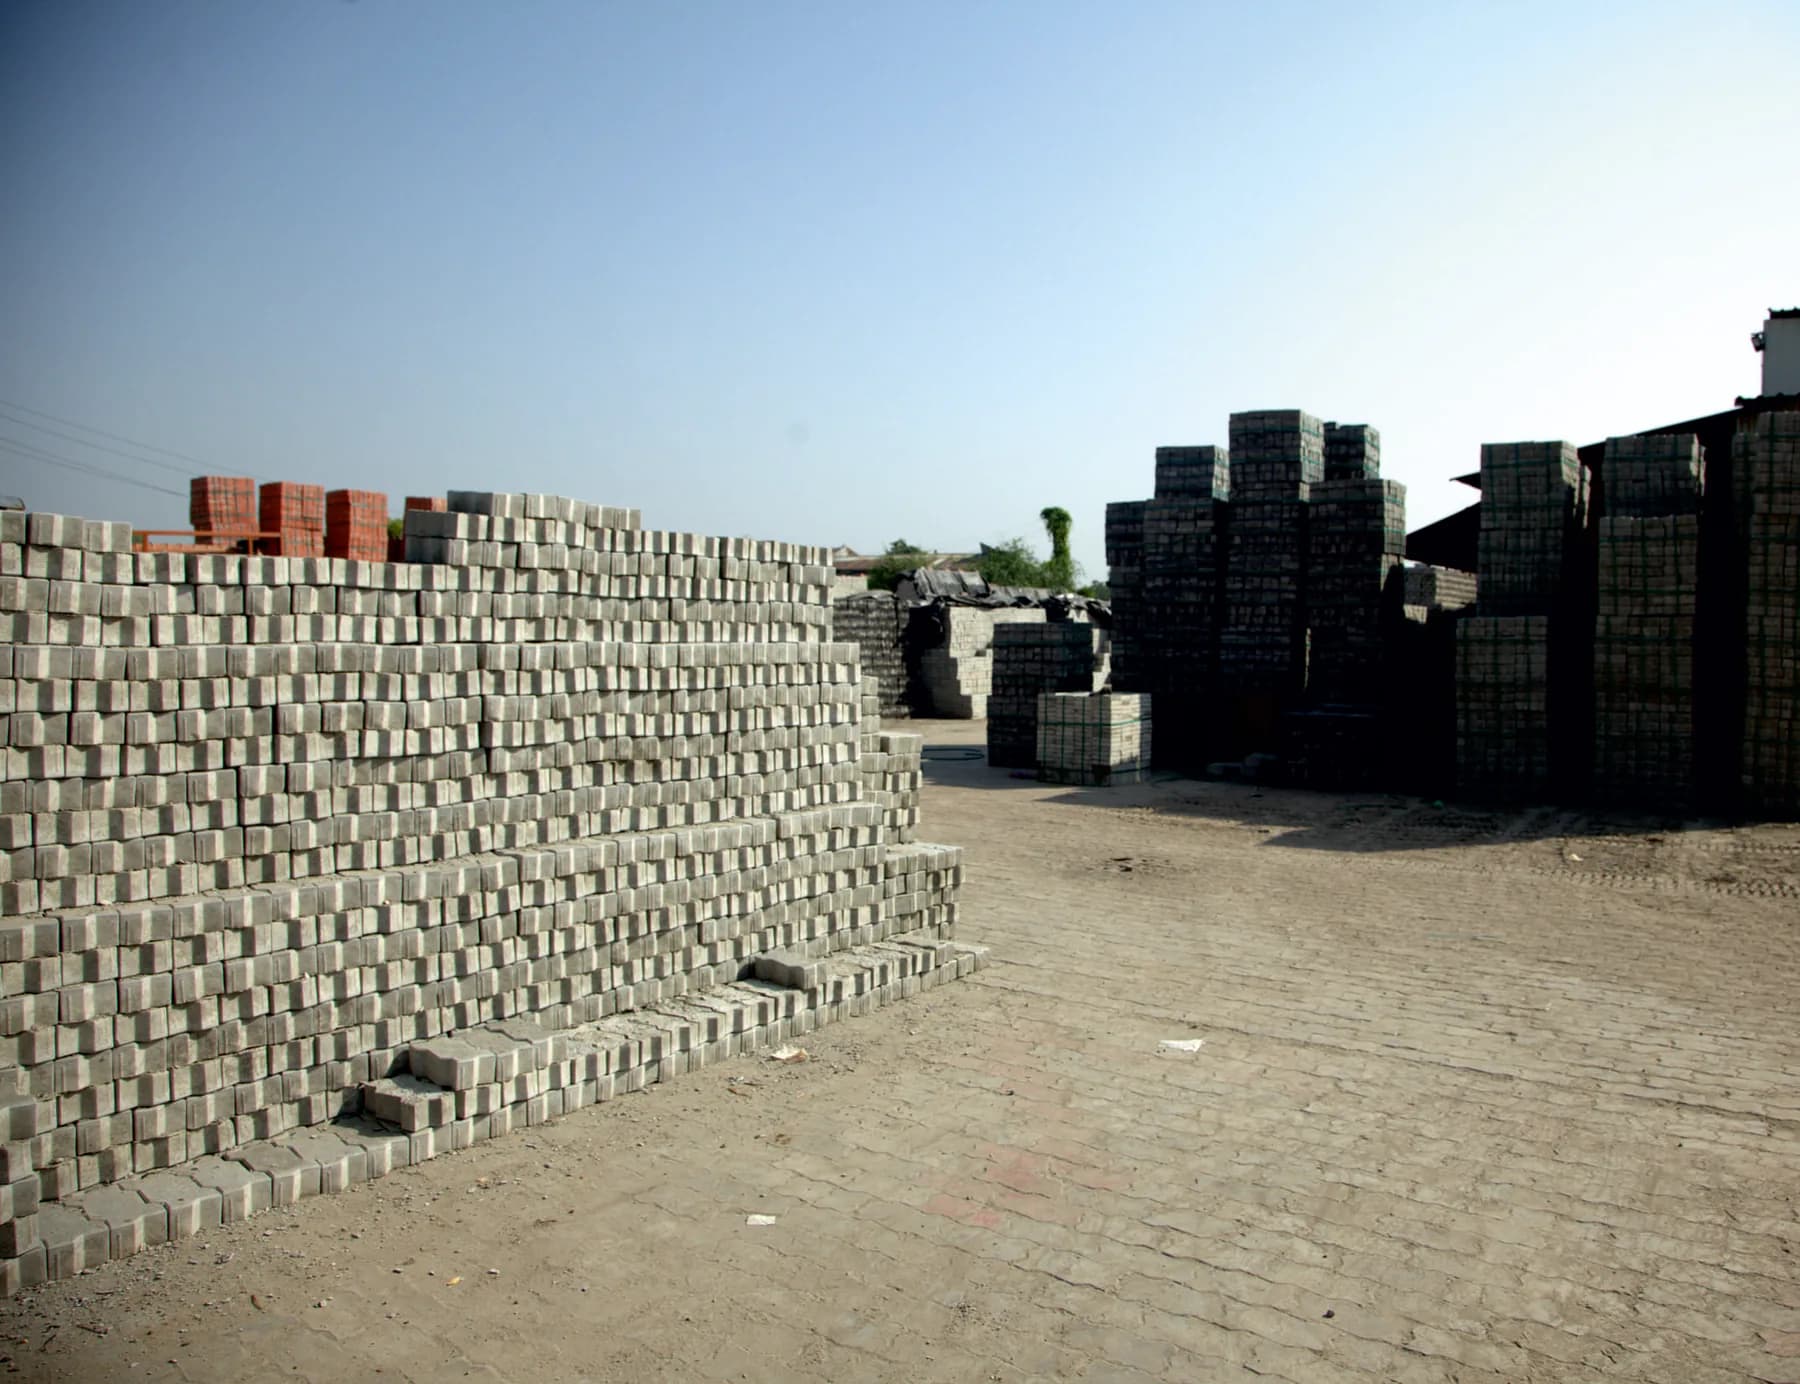
Manufacturing Infrastructure
1,50,000 sq.ft manufacturing area for production and stockyard.
2
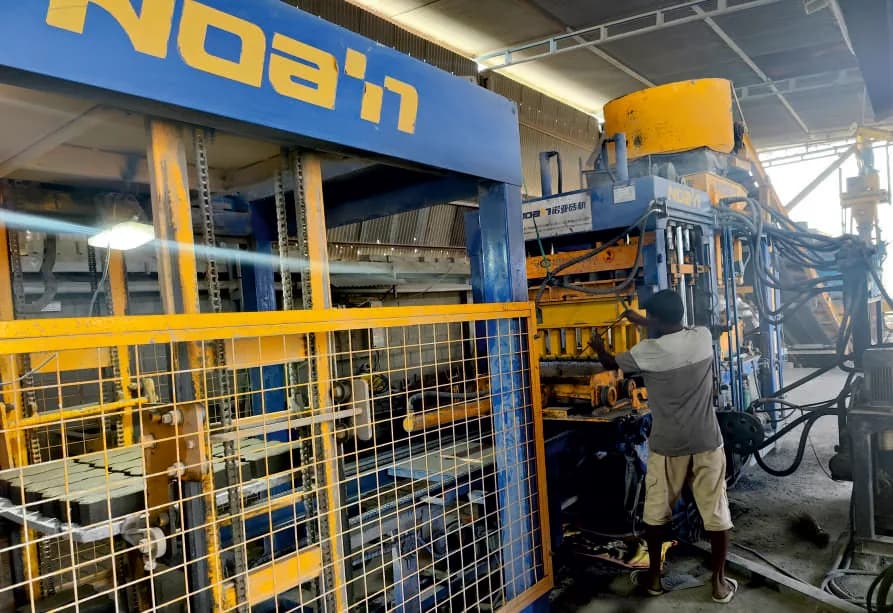
Automated Production
A fully automated production unit with steam curing keeps every batch accurate and consistent, cutting out the human error that comes with manual handling.
3
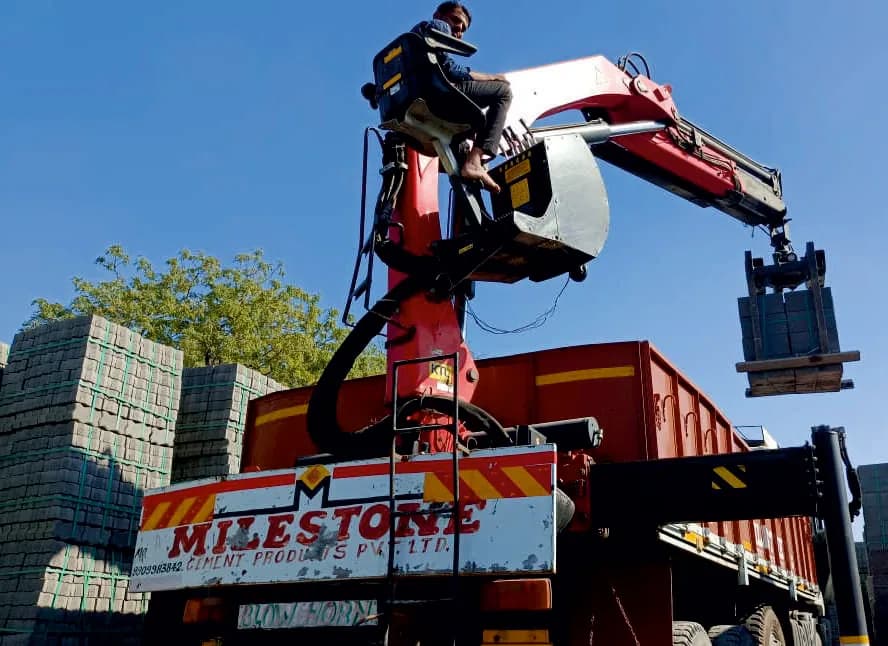
Material Handling
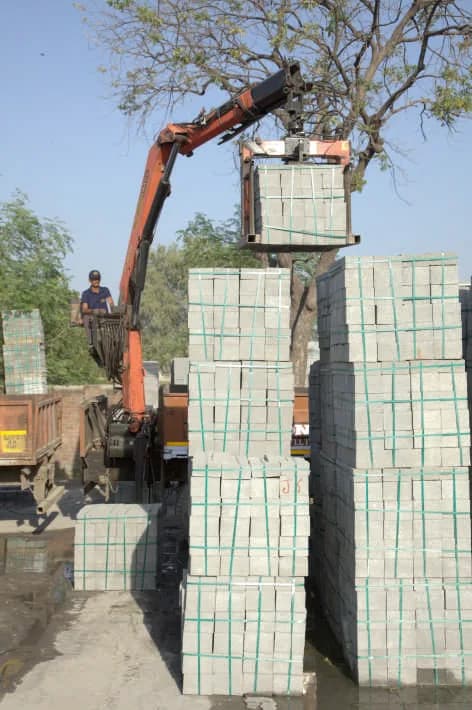
Finished products move through an automatic Palfinger crane for loading and unloading, keeping handling consistent from production line to delivery truck.
4
Production Capacity
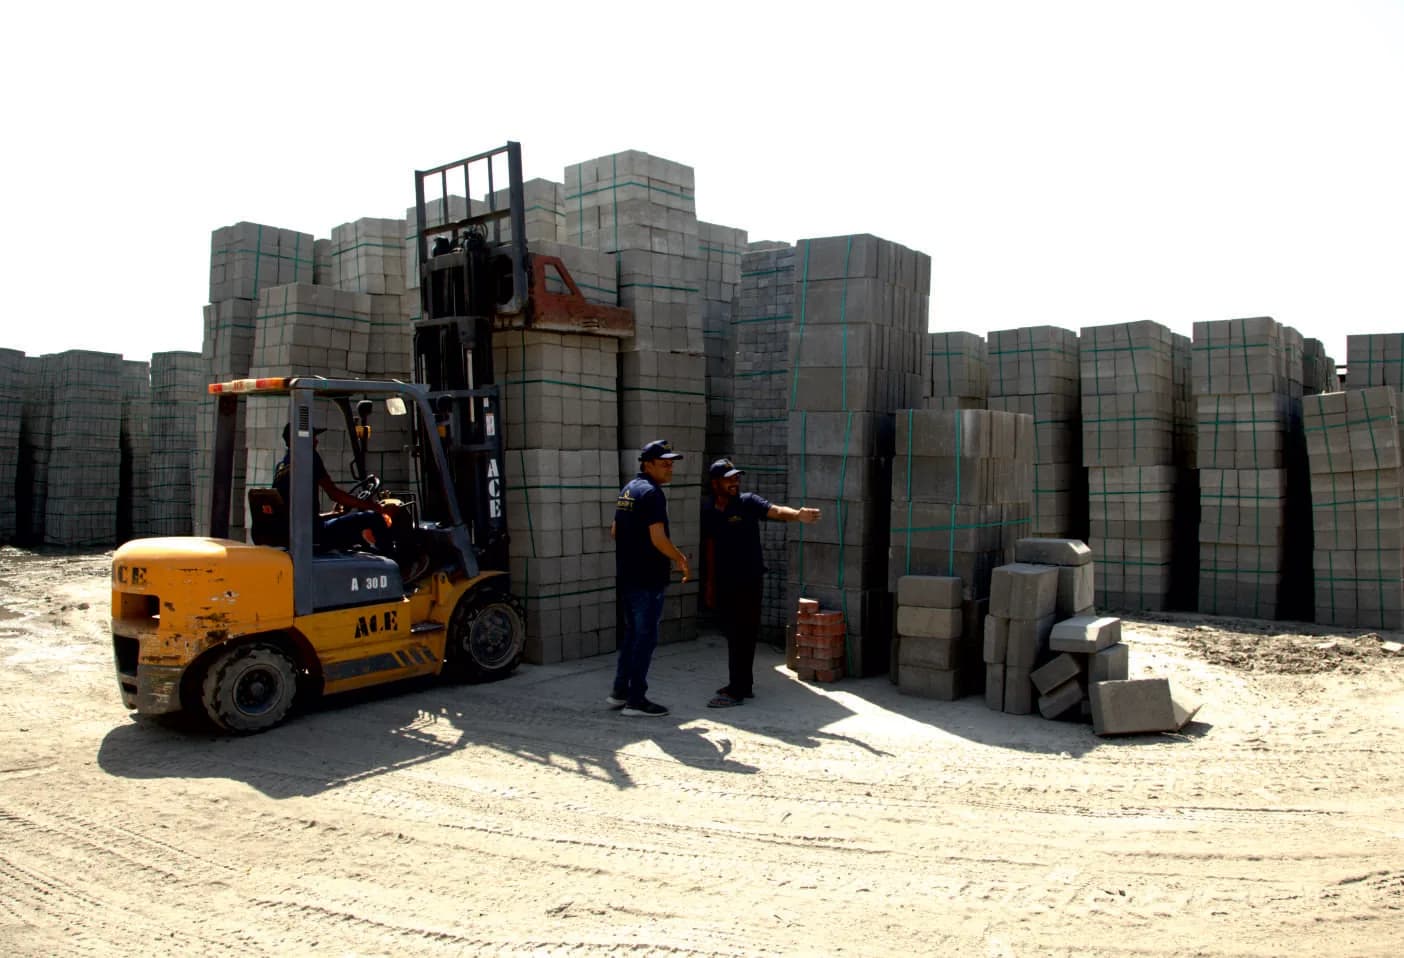
50,000+ pieces produced daily, supported by a 100+ strong team and 6 trucks for transportation.
5
Quality Control
Quality checks run at every stage in our in-house laboratory, including water absorption testing that protects the strength, colour and design retention of every product, backed by expert analysts.
Frequently Asked
Questions
Want the full technical picture? See our quality standards and testing criteria.
Every Milestone product is manufactured in-house at our own 1,50,000 sq.ft factory in Bavla, Ahmedabad — we don't outsource or white-label.
Steam curing speeds up and controls the concrete curing process in a fully automated production unit, keeping every batch accurate and consistent rather than relying on manual handling.
Every batch passes through our in-house laboratory, where expert analysts run quality checks including water absorption testing to protect the strength, colour and design retention of the finished product.
Finished products move through an automatic Palfinger crane for loading, and our own fleet of delivery trucks and 100+ strong team support supply for both small and bulk orders.
Our factory produces 50,000+ pieces per day, giving us the capacity to support large commercial, industrial and infrastructure projects on a set timeline.